Author name: Team Solarkaz

Transportation of goods

Transportation of Goods

Definition The process of moving any equipment from one point to another is defined as transportation. It includes safe, efficient, reliable, and sustainable movement of goods over time. Transportation Role in Logistics Transportation takes a crucial part in the logistics operation. The quick, responsive, and on-time operation of transportation determines the efficiency of moving products. The progress in techniques and management principles improves the moving load, delivery speed, service quality, and operation costs. A healthy transportation system within a country is beneficial in combating bad circumstances by providing timely help in terms of charity work. It is also the corporate social responsibility of organizations to maintain a sustainable transportation system based on renewable energy sources to avoid pollution. Importance of Transportation No equipment deliverables are possible without transportation; hence transportation is a basic core of Logistic operation as well: Without well-developed transportation systems, logistics could not bring its advantages into full play. The On-time transport systems in logistics activities could provide better logistics efficiency, reduce operation costs, and promote service quality. A well-managed logistics system could increase both the competitiveness of the government and enterprises. Principles of Transportation Types of Transportation Rail Transport Advantages Convenient for travelling long distances. Relatively faster than road transport. Suitable for carrying heavy goods in large quantities over a long distance. Less affected by adverse weather conditions like rain, floods, fog, etc.  Limitations Relatively expensive for carrying goods and passengers over short distances. Not available in remote parts of the country. Provides service according to fixed time schedule and is not flexible for loading or unloading of goods at any place. Road Transport Advantages Relatively cheaper mode of transport as compared to other modes. Goods can be transported at a faster speed by road carriers over a short distance. Flexible mode of transport as loading and unloading is possible at any destination. It can provide door-to-door service. Limitations Limited carrying capacity. Road transport is not economical for long-distance transportation of goods. Transportation of heavy goods in bulk by road involves high costs. Water Transport Advantages Relatively economical mode of transport for bulky and heavy goods. Safe mode of transport with respect to the occurrence of accidents. It promotes international trade. Disadvantages The depth and navigability of rivers and canals vary and thus, affect the operations of different transport vessels. It is a slow-moving mode of transport. It is adversely affected by weather conditions. Air Transport Advantages Fastest mode of transport. Very useful in transporting goods to the area which are not easily accessible by any other means. Most convenient mode of transport during natural calamities. Disadvantages Relatively most expensive mode of transport. Not suitable for transporting heavy and bulky goods. Affected by adverse weather conditions. Not suitable for short-distance travel. In case of accidents, it results in heavy losses of goods, Problems Related to Transportation Financing Congestion of routes Infrastructure issues Safety of personnel & equipment Goods weight Height of equipment Local Regulations Country political conditions Weather conditions Transport Costing The following factors are considered during transportation costing: Minimum Weights Loading and unloading locations Packaging Damage in Transit Services charges Insurance Cost Conclusion Transportation and Logistics systems have interdependent relationships in that logistics management needs transportation to perform its activities meanwhile, a successful logistics system could help to improve the traffic environment and transportation development. Since transportation contributes the highest cost among the related elements in logistics systems, the improvement of transport efficiency could change the overall performance of the logistics system. Transportation plays an important role in logistics system and its activities appear in various sections of the logistics processes. With0ut the linking of transportation, a powerful logistics strategy cannot bring its capacity into full play. Solarkaz International provides different industrial equipment including water treatment plants, Boilers, and Heat Exchangers and provides transportation of these equipment to the local and international market and industries. Solarkaz also provides different services including testing and calibration of pressure vessels, heat exchangers, fuel oil tanks, storage tanks and boilers etc. Do you want to know more about the transportation of Goods? Contact us to know more about the controlling process of logistics. #transportation #Roadtransport #Airtransport #Watertransport #solarkaz #solarkazinternational  

Transportation of Goods Read More »

CSR

How Solarkaz Is Serving Pakistan Under Its Corporate Social Responsibility

Solarkaz aims to empower women. But How? Businesses that engage in corporate social responsibility work to better the environment, the economy, and local communities. Corporate social responsibility, or CSR, is a type of self-regulation that demonstrates a company’s accountability and commitment to advancing the social and environmental well-being of communities and society. The four different CSR initiatives that a corporation might use are volunteer work, charitable work, ethical labor practices, and environmental initiatives. This article is for demonstrating to our customers how Solarkaz International maintains high standards of corporate social responsibilities. The success of a company does not count only on extended profitability, pace of expansion, and brand awareness; this is not the only way by which customers, employees, and other stakeholders evaluate a company today. Other factors also count in the success of a company and among the important factors, CSR is one. Almost half of all consumers are turning to brands to set an example for improving the world. Not just customers anticipate this; according to a Glassdoor survey. 75% of employees between the ages of 18 and 34 do as well. Businesses today are held to enormous levels of responsibility and influence. Solarkaz not only understands this but is taking continuous steps for developing strategies to implement CSR, considering it as its ethical responsibility. How Solarkaz Is Implementing CSR? Environment Protection Agency Code of Conduct The Pakistan Environmental Protection Agency is an executive agency of the Government of Pakistan managed by the Ministry of Climate Change. The agency is charged with protecting human health and the environment by writing and enforcing regulations based on laws passed by Parliament. Solarkaz completely complies with all the local requirements of the Pakistan Environment Protection Agency. How are we doing that? Being well aware of the damages that the flue gasses from the boiler could cause to the environment, we don’t release the waste flue gasses directly into the open atmosphere, Instead, we use cyclone filters to filter out all the NOx and SOx-generating elements and flush them out through proper channel from the boilers. Also, we provide economizers in our boilers which take up the heat from the flue gasses for pre-heating the water. Through this, we are also reducing the need for fuel which is potentially helpful for the environment as well. Protecting The Environment By Avoiding Wood Cutting Our environment is too much affected by wood cutting because forests play an important role in reducing the greenhouse effect and purifying the environment. Using wood as fuel for our Boilers is damaging our forests, and ultimately our environment. Solarkaz plays an important role in this regard to bridge the gap and is providing the fuel which is obtained from the leftover after harvesting of crops, hence mitigating the need to cut down the forests for using it as fuel for Boilers. Women Empowerment Solarkaz aims to empower women. But How? Usually in rural areas, farming and harvesting are done by women. While harvesting it is seen that the leftover material like husks, stalks and leaves are of no use to farmers, but they are a potential source of fuel for Bio-Mass boilers. So, Solarkaz provides rural areas women with the opportunity to earn money by selling those leftovers to the nearby facilities of Solarkaz. This helps them develop financially. Volunteer & Charitable Work Solarkaz understands the responsibility for providing Charity and voluntary services whenever it is needed. In the recent flood situation in Pakistan due to the heavy monsoon rainfall, when approximately more than half of Pakistan was suffering from the crises of Shelter and Food supply. Solarkaz came forward and put up its role in providing Shelter and Food to needy families who have potentially lost their homes during this situation.   For this, we collaborated with different government bodies as well. Solarkaz helped flood-affected areas of Khairpur Sindh, along with the Lal Baagh foundation because we believe in helping and building communities in the time of need as our CSR. Conclusion As the world is moving towards low carbon emission solutions, more focus is being transferred towards the role of companies in understanding and implementing their role in entertaining social responsibility. Solarkaz‘s advanced tech will help you in achieving the desired goal. As part of its corporate social responsibility, Solarkaz is actively serving Pakistan by contributing to various social causes. In addition to its commitment to the community, Solarkaz ensures efficient transportation of goods, guaranteeing timely and secure delivery. Let’s explore how Solarkaz combines its CSR initiatives with reliable transportation services for a positive impact. Contact us to know more about the role we are playing to fulfill our corporate social responsibility      

How Solarkaz Is Serving Pakistan Under Its Corporate Social Responsibility Read More »

Biomas-boiler

Why Prefer Solarkaz for Biomass Boilers?

Certified Boiler Manufacturer Solarkaz is a certified manufacturer of Boilers, Pressure Vessels & Heat Exchangers. It has local licenses from the Ministry of Industries & Ministry of Explosives, and from International organizations like the American Society of Mechanical Engineers (ASME), the National Board of Boiler and Pressure vessel inspection (NBBI), the American Welding Society (AWS) and ISO 9001, 14001, 45001 certifications. In Pakistan, it is the only certified Boiler Manufacturer complying with all the local and international requirements for the manufacturing of Boilers specifically Solid fuel fire boilers. Beware of Unauthorized and Illegal Boiler Alteration Shops Everyone must have the market knowledge of the local manufacturers to know why their fabricated Boilers are dangerous. Some of the reasons are given below: No internal or external audits of their fabrication facilities. Having no certifications from international organizations, hence they don’t follow the safety fabrication protocols and standards. Re-using the old material for Boiler fabrication is extremely dangerous for the facilities. Mostly consuming the used pressure vessels and converting them into the Biomass boilers. Not efficient fuel quality used for Biomass boilers. (Only conventional fuels e.g: wood logs that are hazardous for environment. etc.) No warranties and aftersales services for boilers. Benefits of Using Solarkaz Biomass Boiler Over Local Market Boilers Using Solarkaz products has the following benefits: Solarkaz is an internationally certified Boiler manufacturer, several International and Locals audits are being conducted within the fabrication facility to maintain the updated market standards. Solarkaz only uses new and fully tested materials for the fabrication of our Biomass boilers. We also provide our customers with the respective MTCs of the fabrication material for their ready reference. Our Biomass fuel is very efficient, cost-effective and environmentally friendly than the other conventional fuels in the market. Biomass fuel includes Biomass Pellet, wood, Waste Cloth, Rice Husk, Peanut Shell Bagasse, Bamboo Chip Mustard Stalk, Wood Chip, cotton seed, corn cob, Cotton Stalk, etc. We provide a separate cyclone filter in our Biomass boiler design, which enables the system to filter exhaust gasses from the boiler by reducing SOX and NOX emissions, making it environment-friendly as per local & international standards. Solarkaz also provides unmatched warranty for its Biomass Boiler. Solarkaz Biomass boilers are up to 89% efficient. We claim that 310 Kg of our Biomass fuel can produce up to 1 ton of steam. Solarkaz Solutions for Biomass Boiler Our Business model for Biomass boilers is as follows: Turnkey Solution Model: Turnkey solutions are solutions that are completely deployed in a business, effectively fulfilling the need of the client and the client can simply “turn the key” to get started. Solarkaz provides Turnkey solutions for Biomass Boilers to our clients.  Offerings In the turnkey solution model clients get the following benefits from Solarkaz: ✔️ Survey and feasibility visit of client site ✔️ Design & Fabrication of Bio-Mass (Boiler) Package. ✔️ Transportation and Installation of Bio-Mass (Boiler) Package to the site. ✔️ Training of the staff members for proper operation of the Bio-Mass (Boiler) Package. Operations Model: Build Operate Transfer (BOT) Model: BOT is a model that is a contractual relationship in which the client hires Solarkaz to fabricate, set up, optimize, and run Biomass Boilers on their facility. Within this model Solarkaz has contractually stipulated intent of transferring the operation to the organization as a captive center. The instalment period would be 3 Years. RentalIn this model, Solarkaz offers a mutual contract with the client on the consumption/utilization/selling of steam. Initial investment cost could be mitigated through this model. Biomass Fuel Supply Model: This model is intended to supply Biomass boiler fuel only to any biomass boiler of the client. Conclusion Solarkaz is a certified boiler manufacturer having various local and international licenses for the quality manufacturing of boilers, pressure vessels, and Heat Exchangers. Local boilers can be dangerous for both business and human safety because of low quality and refurbished material usage. You can have several benefits by preferring Solarkaz biomass boilers which are mentioned above.   As the world is moving towards low carbon emission solutions, Solarkaz ‘s advanced technology will help you in achieving the desired goal. Solarkaz offers multiple solutions and packages to satisfy any type of customer need with our new biomass boilers that are designed to operate at peak performance while providing high levels of efficiency. When it comes to biomass boilers, Solarkaz stands out as a preferred choice. Discover everything you need to know about biomass boilers, from their working principles to the benefits they offer. Explore why Solarkaz is the trusted provider for reliable and efficient biomass boiler solutions.

Why Prefer Solarkaz for Biomass Boilers? Read More »

WHR-boilers

Applications, Advantages and Examples of Waste Heat Recovery Systems

What is waste heat? Waste heat is energy that is wasted to the environment and is not taken into use. What is waste heat recovery? The reuse of heat energy that would otherwise be wasted or will be released into the atmosphere, is known as “Waste Heat Recovery” What are the Examples of Waste Heat Recovery? Turbo Charged cars Economizers in Boilers Air Preheaters Regenerators Heat Exchangers Absorption Chiller Steam Thermocompression What are the uses of Waste Heat Recovery in Boilers? One of the most basic types of waste heat recovery are stack economizers, which are frequently used to heat water in Boilers. Heat energy from the gas released during the heating process in the boiler flue gas chamber is used by boiler stack economizers to heat the water that goes into the boiler, which lowers the energy needed to produce steam. The US Department of Energy claims that installing a boiler feed water economizer can increase a boiler’s thermal efficiency and decrease fuel usage by 5% to 10%. These boilers work by drawing heat from a hot fluid, usually a gas, that is created as a byproduct of a chemical reaction but has no inherent value as a chemical or that is the exhaust from a gas turbine or internal combustion engine. Boilers for heat recovery are frequently used in high temperature operations like the production of glass and steel What are the uses of Waste Heat Recovery in Boilers? The ideal option for any industry is Solarkaz waste heat recovery boiler systems. Waste heat systems allow heat that is released into the atmosphere to be recovered and used as extra energy for another operation. The need for more efficient and economical energy use grows as energy prices are rising, all over the world. To ensure long-term improvement of plant performance, quality, and productivity, Solarkaz proudly displays its knowledge in goods and services, amassed in this field over time, and offers a wide range of customized and standardized solutions for waste heat recovery. Every waste heat recovery system is specially developed to meet a particular need. Waste heat recovery systems offer a wide range of applications and advantages in industrial settings, and one effective method for heat exchange is the shell and tube heat exchanger. By understanding the principles of shell and tube heat exchangers, we can explore their practical examples and further appreciate their role in maximizing energy efficiency through waste heat recovery. What are the Advantages of using Waste Heat Recovery Boilers? Environment hence using waste heat recovery keeps waste gases at low temperatures Highest efficiency gain due to integrated economizers Utilities (requiring heat energy) can be utilized nearby these boilers Less use of fuel hence increasing the overall efficiency of the boiler Highly reliable in operation and robust in construction Quick payback returns are achieved Eco-friendlyEnergy which was earlier wasted is utilized. High Return on Investment The payback period for waste heat recovery boilers is less than 2 year, making them an excellent investment opportunity. Waste Heat Recovery Boiler Design According to the needs of the plant, waste heat recovery boilers are made to recover heat from waste flue gases from the exhaust, furnace exhaust, kiln exhaust, incinerator exhaust, etc. to produce steam or hot water. 4 basic parameters shall be considered for designing the waste heat recovery system in Boilers, which are: Type of fuel and its composition Amount of flue gases leaving the exhaust system The temperature of flue gases at exhaust Utilization of waste heat Water tube boilers that use the medium to high-temperature exhaust gases to generate steam include waste heat boilers like the two-pass boiler. There are several different capacities for waste heat boilers, allowing for high flows of gas intakes. Auxiliary burners or an afterburner can be installed to increase steam output when waste heat is insufficient to produce the appropriate levels of steam. Power generation or process heating are two uses for steam. An external superheater must be added to the system to produce superheated steam. Do you want to order a WHR boiler? Contact us to get a quote today!

Applications, Advantages and Examples of Waste Heat Recovery Systems Read More »

Water Treatment

Why Water Treatment Is Necessary?

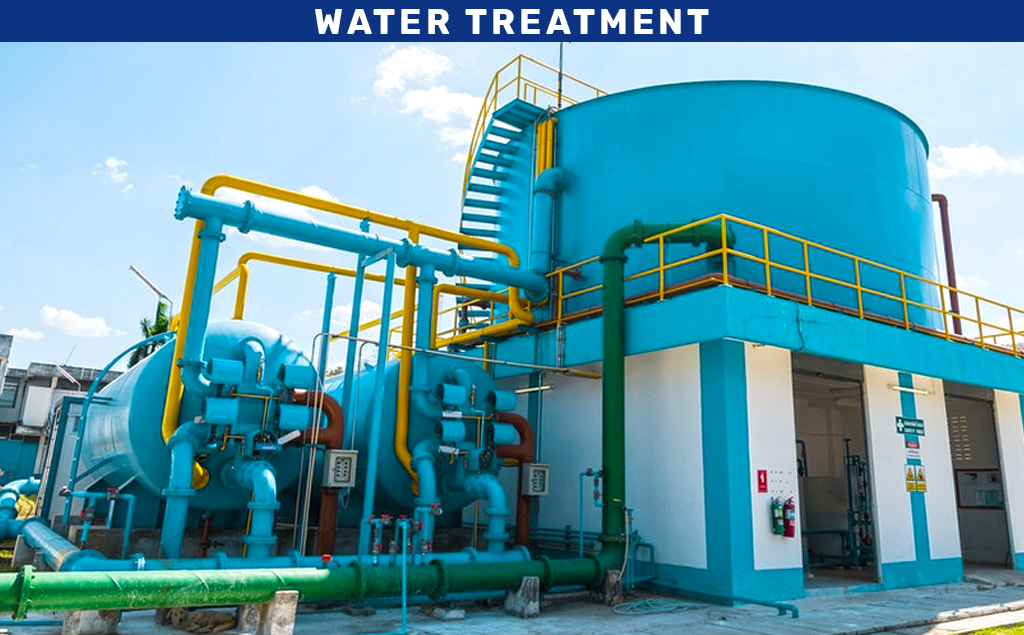
What is Water Treatment? Any procedure that enhances the quality of water to make it suitable for certain end user is referred to as water treatment. The final use could be: ✔️Drinking✔️Irrigation✔️Maintaining river flow✔️Water enjoyment✔️Boilers✔️Heat exchangers To make the water suitable for the intended end use, water treatment involves: ✔️Removing pollutants like oil and different chemicals etc.✔️Unwanted components like dust, mud etc.✔️Reducing the concentration (In terms of ppm). Need For Water Treatment Water is a fundamental need for all living things. It must be pure and untainted. Enough though water covers:  71% of the earth’s surface Only about 1% of it is considered drinkable by international standards due to numerous contamination. Water treatment plays a crucial role in industrial operations, ensuring purity and protecting equipment. Additionally, implementing waste heat recovery systems offers numerous advantages, allowing businesses to harness and utilize valuable energy resources efficiently. Let’s explore how these two essential aspects contribute to sustainable and cost-effective industrial processes. The main causes of water pollution are:  Industrial wastewater discharge Agricultural pollution, Municipal wastewater, Environmental changes, Global warming, Risks to human health, aquatic ecosystems, industrial equipment and the environment exist. The contamination of water causes severe losses to industrial equipment in terms of big disasters and certain property damages. Hence, water treatment is needed to address these issues. Water treatment helps not only in protecting human health but also it helps in protecting industrial equipment from damage. Need For Water Treatment Equipment Water Treatment: Focused on the removal of chemicals causing scale, corrosion and foaming within the equipment like boilers and heat exchangers. Water Treatment for Drinking: For making water drinkable, water is being treated to maintain a certain pH level within the water also a TDS level of water is maintained below 200 ppm. Water Treatment Steps Raw water can be: Groundwater Sea Water (1) Oxygen Scavanging Operation and maintenance of commercial boiler systems and steam-generating plants must address the serious problem of oxygen-related metallurgical corrosion. This can be achieved using carefully selected oxygen scavengers designed specifically for steam boiler corrosion control and feed water corrosion control in steam-raising plants. Oxygen scavengers are critical to preventing dissolved oxygen from causing corrosion (called oxygen pitting) in boilers. Mechanical deaeration should remove most dissolved oxygen, but chemical oxygen reduction (called scavenging) is required to provide optimum protection. Oxygen scavengers are designed to reduce (scavenge or destroy) dissolved oxygen, so they can not cause oxygen pitting. The optimum oxygen scavenger is based on system design and steam usage requirements. (2) Coagulation The initial stage of water treatment is coagulation. Positively charged chemicals are added to the water during coagulation. The negative charge of dirt and other dissolved particles in the water is balanced by the positive charge. When this happens, the particles and chemicals bond together to create somewhat larger particles. In this step, common substances include certain: Salts Aluminium Iron. (3) Flocculation Coagulation is followed by flocculation. Water is gently mixed to generate larger, heavier particles known as flocs through a process called flocculation. In order to aid in the formation of the flocs, water treatment facilities frequently add extra chemicals during this phase. (4) Sedimentation A typical method of treating water is sedimentation. It is a method for getting rid of solids in the water that float and settle. Larger particulates are removed from the process using sedimentation tanks. Sedimentation may be followed by further treatments. (5) Filtration The clean water on top is filtered to remove further solids from the water after the flocs have sunk to the bottom of the tank. The pure water goes through filters constructed of various materials and with various pore sizes during the filtration process (such as sand, gravel, and charcoal). These filters eliminate: Germs Dust Chemicals Parasites Bacteria Viruses. (6) Disinfection Water treatment facilities may add one or more chemical disinfectants such as: ✔️ Chlorine✔️ Chloramine✔️ Chlorine dioxide After the water has been filtered to eliminate any lingering parasites, bacteria, or viruses. Water treatment facilities make sure the water has low concentrations of the chemical disinfectant before it leaves the facility to help keep water safe as it goes to residences and commercial establishments. The remaining disinfectant eliminates bacteria that are present in the pipes that run from the water treatment facility to your tap. Conclusion Solarkaz International provides water treatment plants and chemicals to address the issues and challenges that normally industrial equipment face. Solarkaz provides the solution for water treatment by the fabrication of a water treatment plant. It also provides Acid inhibitors, hardness controllers, anti-scaling chemicals, oxygen scavengers, sludge condition chemicals and different anti foaming compounds for protecting industrial boilers from corrosion, scaling and pitting. Do you want protect your industrial equipment from corrosion, and scale formation? Contact us to know more about the water treatment system.

Why Water Treatment Is Necessary? Read More »

How to Prepare Your Boiler for an Inspection

For any industry that uses industrial boilers, boiler inspection is essential. Boilers often operate under extreme conditions of temperature and pressure due to which periodic inspection of boilers becomes necessary to avoid any damage. Without a proper inspection, a boiler is not only a hazard for a facility, but it has the potential to cause fatality and catastrophic failure. Boiler inspections help prevent catastrophic failures by identifying and rectifying those flaws so that boiler operations could become safe and secure. Boilers are often inspected annually, in which they are inspected thoroughly from internal and external sides under no pressure conditions. These inspections are carried out as a part of preventive maintenance which is often performed during the period of the shutdown of a plant. Although, some organizations also require an additional exterior inspection halfway through the year. According to studies, “Increasing the frequency of boiler checks can extend asset life and reduce greenhouse gas emissions, but businesses must measure these advantages against the expense of doing more inspections” Pre-Requisites for Boiler Inspection 🔎 Trained Inspectors  Only well-trained and certified people should be hired for the inspection of boilers.  The inspectors should be aware of the ASME standards of inspection and testing.  Inspectors shall be aware of the safety protocols while inspecting the boilers.  They shall be well equipped with the relevant testing, inspection, and safety equipment. Safety of Inspector 🦺 Safety equipment that shall be required for performing high-pressure boiler inspections includes: A safety hat and safety glasses Safety shoes Gloves Coveralls Flashlight Camera (with a securely closed battery compartment) Inspection mirror Magnet Containers for storing deposits A knife, screwdriver, or another scraping device Any necessary atmospheric testing equipment Any additional advanced testing equipment required Preparation of Boiler for Inspection To prepare a boiler for inspection, the owner should take the following steps, as required by the inspector: Drain water and wash the boiler thoroughly. Remove manhole and hand-hole plates, washout plugs, and inspection plugs in water column connections. Cool and clean furnace and combustion chambers. Remove grates from internally fired boilers. Remove brickwork insulation to determine the condition of the boiler, headers, furnace, supports, and other parts. Remove the pressure gauge. Prevent steam or hot water leakage into the boiler by disconnecting the pipe or valve at a convenient point, or through any other means approved by the inspector. Close, tag, and padlock non-return and steam stop valves before opening the manhole or hand-hole covers. Open drain valves and/or cocks between the two valves. Close, tag, and padlock blow-off valves after draining the boiler. Disconnect blow-off lines between pressure parts and valves when possible. Open all drains and vent lines. Following the Safety Protocols ⚠️ Inspectors should follow all plant safety protocols in addition to possessing the required safety equipment described above and preparing boilers for inspection. Other safety advice comprises:  Examine together or with the assistance of an inspection attendant.  Before the inspection, make sure that all valves, including the feedwater, chemical feed, blowdown, and steam valves, are locked out and turned off.  To make sure the boiler is not excessively hot, measure the temperature of the naked metal.  Use atmospheric monitoring tools to make sure the situation is not dangerous Inspection of Boilers Inspection of the Boiler includes: Checking of Boiler controls including pressure gauges, low water cut-off devices, thermometers, temperature controls, gauge glass and pressure relief valve. Checking the water and fuel internal and external piping conditions of the boiler to ensure it is in good condition and is as per ASME standards. Flue gas pipe connections shall also be reviewed and inspected to ensure that the traces of carbon monoxide are being expelled properly. Visual inspection to check the overheating, corrosion, and erosion on the internal and external walls of the boiler. To visually inspect the burners within the boilers if they are receiving the correct ratio of fresh air for combustion. Testing of all drains and blow-offs to ensure that they are functioning properly. Check the fuel system for leaks and ensure that all fuel filters and strainers have been replaced. Verifying that every shut-off valve is leak-proof and performing a leak tightness test if necessary. Testing that each valve in the instrument line is operating properly. Checking the vent valve on gas-fired boilers is functioning properly and is not obstructed. Checking that the flame scanner or sensors are correctly wired and operational. Verifying all instruments and safety devices are in a proper setting. Checking if the re-circulation pump operates adequately. Checking that all heating system isolation valves are functioning properly. Verifying that there are no leaks from any part of the boiler or piping external to the boiler. Have any cracked surfaces repaired immediately by a qualified repair company. Bulges or other deformities indicate defective controls, safety devices or improper burner operation. Testing safety valves periodically. Replace leaking safety valves. Test safety or relief valves by lifting the test lever at least once a year. Verify that the low water fuel cutoff control shuts off the fuel supply to the boiler as required. Inspect the low water fuel cutoff control for proper sequence and operation. Checking if the isolation coating of the piping is not damaged at any point. Inspectors should assess high-pressure boilers against all applicable regulations and standards, so the specific inspection steps may vary between locations subject to different regulatory guidelines. Conclusion Solarkaz International assists you with your boiler inspection needs. Solarkaz Boiler inspections are performed by Certified API inspectors. Our main concern is ensuring the quality of the boiler as per the latest ASME or relevant code of construction. At the time of performing inspections, Inspectors will examine your equipment and will identify the risks that the boiler may suffer. In addition, the inspector will review the existing condition of the boiler and will make recommendations to ensure that your high-pressure boilers continue to operate safely and comply with all necessary standards. Solarkaz also provide fabrication of Waste heat recovery boilers, Multi fuel fired boiler, Gas fired package type boiler, Wetback package type boiler,

How to Prepare Your Boiler for an Inspection Read More »

Get To Know About Pressure Vessels

Pressure vessels, as defined by ASME Boiler and Pressure Vessel Code (BPVC) Section VIII, are containers for the containment of pressure, either internal or external. The application of heat from a direct or indirect source because of a process, or any combination of the two, can create this pressure. What are ASME codes? ASME is abbreviated as “American Society of Mechanical Engineers”. The ASME Code is the construction standard for pressure vessels and contains standards that must be followed, prohibitions that must be avoided, and mandatory and non-mandatory advice for pressure vessel materials, design, fabrication, examination, inspection, testing, and certification. Types of Pressure Vessels As Per ASME Code Pressure vessels are organized into five types: Type I All-metal construction, generally steel. Type II  Mostly metal with some fiber overwrap in the hoop direction, mostly steel or aluminum with a glass fiber composite; the metal vessel and composite materials share about equal structural loading. Type III Metal liner with a full composite overwrap, generally aluminum, with a carbon fiber composite; the composite materials carry the structural loads. Type IV  An all-composite construction, polymer — typically polyamide (PA) or high-density polyethene (HDPE) liner with carbon fiber or hybrid carbon/glass fiber composite; the composite materials carry all the structural loads. Type V Liner-less, all-composite construction. Types of Pressure Vessels According to Shape 1. Spherical Pressure Vessels High-pressure liquids are best stored in this specific kind of pressure vessel. Because the forces are evenly distributed over its surface, both internally and externally, a spherical construction is exceptionally sturdy. As a result, all weak places are eliminated, but it is also true that making them can be far more expensive than making cylindrical ones. The fact that spherical pressure vessels have a smaller surface area per unit of volume than any other shape is a major advantage. Accordingly, compared to cylindrical storage vessels, the quantity of heat that is transferred to liquid within the sphere from warmer surroundings will be significantly smaller. Spherical vessels make up the majority of LNG (Liquid Natural Gas) and LPG (Liquid Petroleum Gas) tanks. They are also used to hold butane, propane, ammonia, oxygen, hydrogen, and nitrogen. Advantages A spherical shell pressure vessel would be more cost-effective when you need to create storage for a large volume of pressurized liquid or gas, which means you need a massive pressure vessel. Disadvantage  The fabrication cost of spherical shell pressure vessels is higher than that of cylindrical pressure vessels, and only big vessels can justify this higher cost. 2. Cylindrical Pressure Vessels Because cylindrical vessels are less expensive to create than spheres. Cylindrical Vessels are frequently utilized for storage. However, because of the weak spot at either end, cylinders are not as powerful as spheres. By fitting hemispherical or rounded ends, this vulnerability is lessened. Storage pressure can be comparable to that of a sphere if the entire cylinder is constructed from thicker material than a comparable spherical tank of similar capacity. Types of Cylindrical Pressure Vessels According to Head Three different ASME pressure vessel end heads are ellipsoidal, hemispherical, and tori spherical. ✔️ Ellipsoidal Head The 2:1 elliptical head is another name for this. Because the height of the head is just one-fourth its diameter, it has a more practical shape. Between the major and minor axes, its radius changes. ✔️ Hemispherical Head Because the pressure inside the vessel is distributed evenly throughout the surface of the head, a spherical is the best shape for a head. The head’s radius (R) is the same as the cylindrical portion of the vessel’s radius. ✔️ Torispherical head The size of the dish on these heads, which has a defined radius (CR) and varies depending on the type of torispherical head, is fixed. The knuckle is the point where the cylinder and the dish meet. The knuckle is shaped like a torus. Do We Fabricate Pressure Vessels? Solarkaz International is an ASME certified company, with ASME “U Stamp” and “S Stamp” and ISO certifications as well. We fabricate pressure vessels for various industries, including Beverages, Pharmaceuticals, Water & Wastewater, Oil & Gas, Food and health care etc. Discover the importance of water treatment and the role of pressure vessels in ensuring the safety and efficiency of industrial equipment. Solarkaz International offers comprehensive solutions, from fabricating pressure vessels for storage to providing water treatment plants and chemicals for optimal performance and protection.  Looking for pressure vessel solutions? Contact us to know more about the Pressure Vessels.

Get To Know About Pressure Vessels Read More »

10 Boiler Safety Preventions You Should Know

Boilers are the most critical elements within an industry. Specially the boilers that are being used without a standby unit/boiler, having low or no maintenance specially in the case of any fuel other than Natural Gas. What are the Main Causes of Boiler Accidents? Major causes of boiler accidents can be due to failure of pressure parts of steam and water sides, safety valves failure, corrosion and degradation of boiler wall material, loose welded and non-tested joints. The probability of which is very low (ONLY 0.5% OF THE ACTUAL ACCIDENTS) when you get your boiler for an Authorized Manufacturer complying to all the latest code construction of boilers such as ASME SEC I Div.1.   Poor water treatment causing scaling and overheating of the plates, Low water levels, un-trained boiler operator, improper cleaning of the boiler furnace (WHEN IT COMES TO BIOSMASS FIRED BOILERS). According to inspection records of various sources in the U.S., UK, and Europe in the late 19th and early 20th centuries the weakening of boilers due to simple scaling both water side and fired side was the most frequent cause of boiler accidents. Also nowadays many unauthorized and illegal boiler alteration shops are manufacturing boilers which are very harmful, not only for the company also for the lives of the people as they are prone to catastrophic explosions. Hence, while buying boilers one should consider the certified boiler manufacturers over the local manufactures. For clear understanding of failure associated with the boilers, an Ishikawa diagram for the root cause failure analysis of a steam boiler failure is shown below:   Some of other related failure causes are as follows: Pressure Vessel Failure (OPERATIONAL ERROR / UNTRAINED STAFF) The most common reasons for pressure vessel failure are excessive scale formation both water and fire side, low water levels, or corrosion or overheating of the metal. Damaged safety valves or water hammer may also have an effect on the vessel. When the vessel’s pressure range is compromised, it happens. To better grasp it, consider that a steam boiler working at 100 psig may expand water by a factor of 1500 from its initial volume. As a result, it generates a powerful force that results in dangerous boiler accidents.       Boiler Corrosion Untreated water contains a sizable amount of dissolved oxygen, which is a major contributor to corrosion. The oxidation, scaling, and corrosion processes are accelerated by the high heat intensity of evaporation. Pitting corrosion causes boiler tube failures and may harm the equipment farther downstream. Accidents Due to Scaling on Furnace of Water Tube Boiler Running on Solid Fuel / Biomass It is observed that when a boiler is operated on any solid fuel or biomass and the quality of the fuel is not controlled; unwanted deposits start to occur on the surface, walls of the furnace which results in poor heat transfer. If the boiler furnace is not properly cleaned than this results in overheating of the boiler resulting in hardness in material and cracking of water wall tubes of the furnace. This is the most common accident that is faced by companies who have untrained boiler operational staff. Accidents Due to Choking of Furnace of Boiler Running on Solid Fuel / Biomass It is observed that when a boiler is operated on any solid fuel or biomass and the quality of the fuel is not controlled i.e. sand, plastic or any item that has a higher melting point or cannot be burned other than the fuel being used for e.g. the roots of the tree the air nozzles on the bed of the furnace get chocked. If not properly cleaned that this will result in the overheating of the furnace bed of the boiler and ultimately result in a severe accident of the boiler. This is also a common accident that is faced by companies who have untrained boiler operational staff Prevention of Boilers From Explosion Following are some of the key parameters that can prevent Boilers from explosions: Regular Checking of Safety valves Proper insulation of heated parts of the Boiler Pressure Gauge monitoring Boiler ash tray and tubes cleaning on periodical basis to prevent them from scale formation Periodic maintenance of Boilers Proper treatment of Water before entering into the Boiler Boiler should not be operated at or above the maximum allowable pressure limits Boiler vents checking Check for LEL level and fuel line leakages before the ignition Trained and educated operational staff (most important)

10 Boiler Safety Preventions You Should Know Read More »

Let’s Talk About Shell and Tube Heat Exchanger

The heat exchanger is used for transferring heat from one medium to another medium. A heat exchanger acts as a cooler or warmer for a fluid and it can be used in many different applications such as power plants, refrigeration systems, air conditioning, and heating systems, mining systems, and food industries. Today many of the industries are even using waste heat recovery systems in boilers which also serve the purposes of heat exchanging between two systems for example, the outlet of the boiler is connected with the economizer to enhance the overall efficiency of the boiler. Hence, heat exchangers are very beneficial for any industry. The Shell & Tube Heat Exchanger is a solid-wall heat exchanger with a proper shell and tube-type structure. It operates with a top and bottom loop of tubing and has two fluid passages through the core. This design allows heat transfer without an intermediate step in between the heat source and multiple destinations, making it more efficient than other types of heat exchangers. Classification of Heat Exchangers by Flow Configuration Cocurrent Flow In cocurrent flow type heat exchanger, the streams flow parallel to each other and in the same direction. This is less efficient than countercurrent flow but does provide more uniform wall temperatures. Cross Flow Crossflow heat exchangers are intermediaries in efficiency between countercurrent flow and parallel flow exchangers. In these units, the streams flow at right angles to each other Countercurrent Flow Countercurrent flow exchanger is one in which the two fluids flow parallel to each other but in opposite directions. This type of flow of arrangement allows the largest change in temperature of both fluids and is therefore most efficient. Cross/Countner Flow In counter flow type of heat exchanger, the two fluids flow parallel to each other, but in opposite directions. Why Baffles Are Used In Shell and Tube Heat Exchangers? ✔️ To support the tube✔️ To direct the fluid stream across the tube✔️ To improve the rate of heat transfer Advantages of Heat Exchanger ✔️ High Efficiency✔️ High operating pressures✔️ More heat transfer between the different sources✔️ Less Costly than others Limitations of Heat Exchanger ✔️ Large size✔️ More space is needed for cleaning✔️ Difficult to clean Shell Side Heat Exchanger Problems 1. Heat Exchanger Fouling Fouling is the formation of unwanted material deposits on heat transfer surfaces of tubes during process heating and cooling. Fouling might contain materials that consist of either living organisms or non-living organisms. Types of Fouling ✔️ Incrustation✔️ Scaling✔️ Sediment✔️ Biological Growth Reasons of Fouling ✔️ Variable water pH ✔️ Product viscosity ✔️ The Roughness of component surfaces Solutions ✔️ Using cleaning agents for removing the scaling and incrustation ✔️ Removing sediments ✔️ Using a chemical cleaning process or water treatment method to remove biological growth 2. Corrosion Corrosion is the gradual deterioration of metals caused by the action of air, moisture, or a chemical reaction (such as an acid) on their surface. Solution Selecting the material with adequate corrosion resistance for the environment along with using proper treatment chemicals. 3. Vibration Heat exchangers should not be placed near equipment such as air compressors or mechanical chillers because excessive vibrations from these machines can cause tube failures. Conclusion Shell and tube type heat exchangers are used widely in the industrial market and are the most commonly available heat exchangers within the markets due to the high demands. Also, the maintenance of these heat exchangers is very easy compared to the other heat exchangers. Solarkaz International is providing the best solution for Heat Exchangers throughout the markets, which is valuable in regard to the total cost of ownership. We had several clients all over the world, and we are competent in building Heat Exchanger designs as per International Standards. Looking for the Heat Exchangers? Contact us to know more about the Heat Exchangers.

Let’s Talk About Shell and Tube Heat Exchanger Read More »

Everything You Need to Know About Biomass Boiler

Biomass which is the renewable energy source of organic material is now an emerging source of fuel used worldwide for power boilers.   Advantages of Biomass As Fuel Biomass can be used for several industrial and domestic purposes as well as is useful as boiler fuel. Biomass is being used as an effective alternative to traditional coal, petroleum coke or oil, and gas fuels. Biomass has a low impact on the environment compared to conventional fossil fuels. This type of energy production has a limited long-term effect on the environment because the carbon in biomass is part of the natural carbon cycle, while the carbon in fossil fuels is not, and does not permanently adds carbon to the environment as compared to the burning of conventional fuels. Some of the advantages of Biomass fuel in boilers are as follows: Environmentally friendly, non-polluting, and non-hazardous fuel Produces low Carbon footprints Widely available Produced and degraded easily as compared to the availability of oil and gas reserves which are being depleted at the faster pace Less expensive. Types of Biomass Fuels Biomass fuel is produced from a wide range of materials. These burning fuels include wood, agricultural residues, animal manure, and organic wastes from households and industries. Want to Know About Biomass Boilers? Biomass boilers are very similar to gas boilers but use several types of organic compounds like Biomass Pellet, wood, Waste Cloth, Rice Husk, Peanut Shell Bagasse, Bamboo Chip Mustard Stalk, Wood Chip, cotton seed, corn cob, Cotton Stalk, etc. as fuel sources. The conventional life cycle of working of biomass boilers employs: The sources of fuel are first converted to pellets. These pellets are then transported to the industries for feeding into the biomass boilers. The pellets are fed into the automatic feed hopper of the biomass boiler which stores pellets and feeds them into the boiler when needed.   After combustion of the fuel, the fuel ashes are accumulated into the ashtray from where they are removed as per the instructions of the boiler manufacturer. Wrong Perception Some people have the idea that biomass boilers are labor intensive, due to the traditional perception of how they work. In the past, people thought that they needed to fill up the boiler every day and clear it out occasionally to ensure that it worked properly.  This is no longer the case with modern biomass boilers, as they can provide clean, efficient, and technological solutions for the needs of the modern world. But still safety and prevention of boilers is necessary in terms of its use, because if the boilers are not properly maintained and cleaned there exists a chance of boiler eruption which could be catastrophic. This is no longer the case with modern boilers and biomass boilers, as they can provide clean, efficient, and technological solutions for the needs of the modern world. Being Futuristic Nowadays, biomass boilers are engineered in a way to reduce labor while providing a fully automated system of feeding, bed functioning, exhaust gas emissions, and fan-forced or natural draft mechanism as per international standards and provide space flexibility for various fuels within the feeding chamber of the boiler. Solarkaz International has expertise in manufacturing biomass boilers which could provide all of the above features with a fully automatic control system and additional safety and reliability. Our aim is to provide a quality product to our clients at economical prices. Looking for the Biomass Boilers? Contact us to get FREE enquiry about Biomass Boilers.

Everything You Need to Know About Biomass Boiler Read More »